


Capabilities
Machinery
MCS runs its own CNC fibre laser, CNC V-grooving machine and CNC press brake in a 20,000 sq ft workshop in Narela. Tolerances and performance data are given for each enquiry, against your section.

On film
The machines
at work
A silent clip from the shop floor: our fibre laser cutting a stainless steel sheet on the 2 × 4 m bed.
Filmed in our workshop in Narela, Delhi. The clips are silent and play while on screen; tap one to pause it.
In the workshop
Machine list
| CNC Fibre Laser | 2 m × 4 m bed. Cuts large sheets for profiles, perforation and pattern work. |
|---|---|
| CNC V-Grooving | Up to 4 m long. Grooves long sheets for architectural profiles. |
| CNC Press Brake | 5-axis, bends up to 3 m long. Bends long architectural sections under CNC control. |
| Welding | TIG and spot welding stations, for assembly and sub-assembly. |
| Finishing | Deburring, grinding, buffing, polishing and bead blasting. |
| Sheet thickness | 0.25 to 4 mm, in stainless steel, mild steel, aluminium, brass and copper. |
Tolerances and performance data are given for each enquiry, checked against your actual section.
Will my part fit?
Check your part against
our machines
The limits that decide most job work. Tolerances, minimum flanges and groove depths are confirmed for each enquiry, against your section and metal.
Sheets up to 4 m long
For sharp corners on long profiles, trims and cladding. Send the section with its leg lengths.
5-axis CNC press brakeBends up to 3 m long
For multi-bend sections, channels and boxes. Send the bend angles and the order you need them in, if you know it.
CNC fibre laser2 m × 4 m bed
For blanks, perforation and patterns, cut flat before bending. Send a DXF if you have one.
Sheet thickness0.25 to 4 mm
Bent and V-grooved, in stainless steel, mild steel, aluminium, brass and copper. Laser cut up to 16 mm mild steel and 8 mm stainless steel. Say the metal and the grade.
Workshop20,000 sq ft in Narela, Delhi
Design desk, laser, V-grooving, press brake, welding, finishing, inspection and dispatch under one roof.

CNC fibre laser · 2 m × 4 m bed
Every part starts
as a flat blank
The fibre laser cuts the flat blank of a part before it is grooved or bent: the outline, holes, slots, notches, perforation and decorative patterns, straight from a DXF file.
Parts are nested together on the sheet to use the metal well, and every hole and notch is cut in the same set-up as the outline, so holes and bend lines stay where the drawing puts them. The 2 m × 4 m bed takes a full 4 × 8 ft sheet.
Used for: blanks for profiles and panels, perforated façade and ceiling panels, laser-cut screens, brackets and plates.
CNC V-grooving · sheets up to 4 m long
The groove that makes
the sharp corner
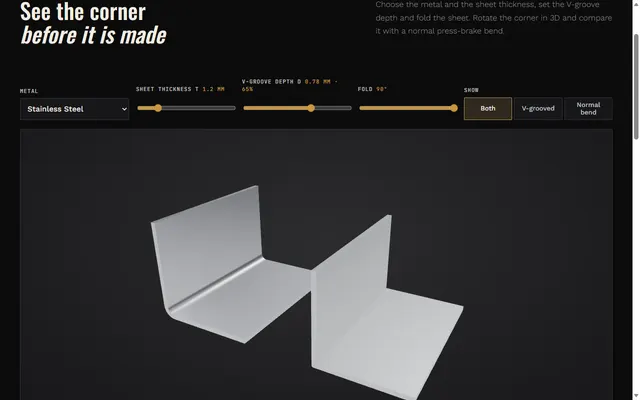
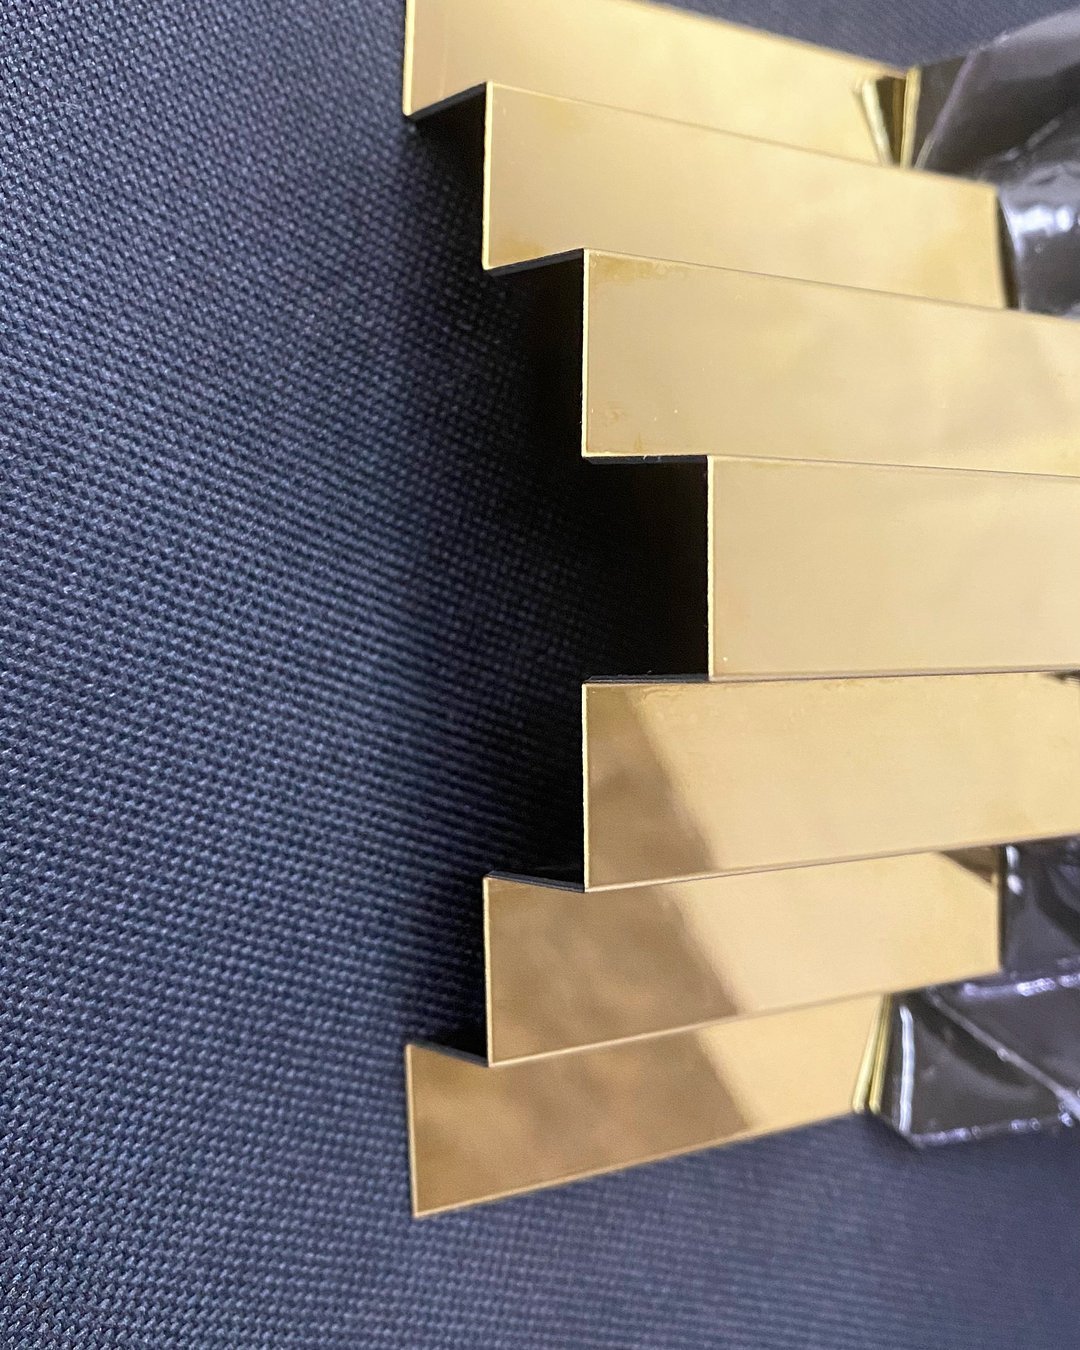
Before a sheet is bent, the V-grooving machine cuts a V-shaped groove along each bend line on the back of the sheet, leaving a thin web of metal. Folded on the press brake, the corner closes to a crisp edge instead of a round bend.
Pneumatic clamps hold the sheet flat along its full length while the tool runs the groove, and the groove depth is set for the metal and the thickness. Sheets up to 4 m long are grooved in one piece, so long trims, columns and cladding have no joint.
Used for: architectural profiles and trims, lift and column cladding, panels with sharp returns, signage and furniture edges.

5-axis CNC press brake · bends up to 3 m long
Folded in the right order,
every piece the same
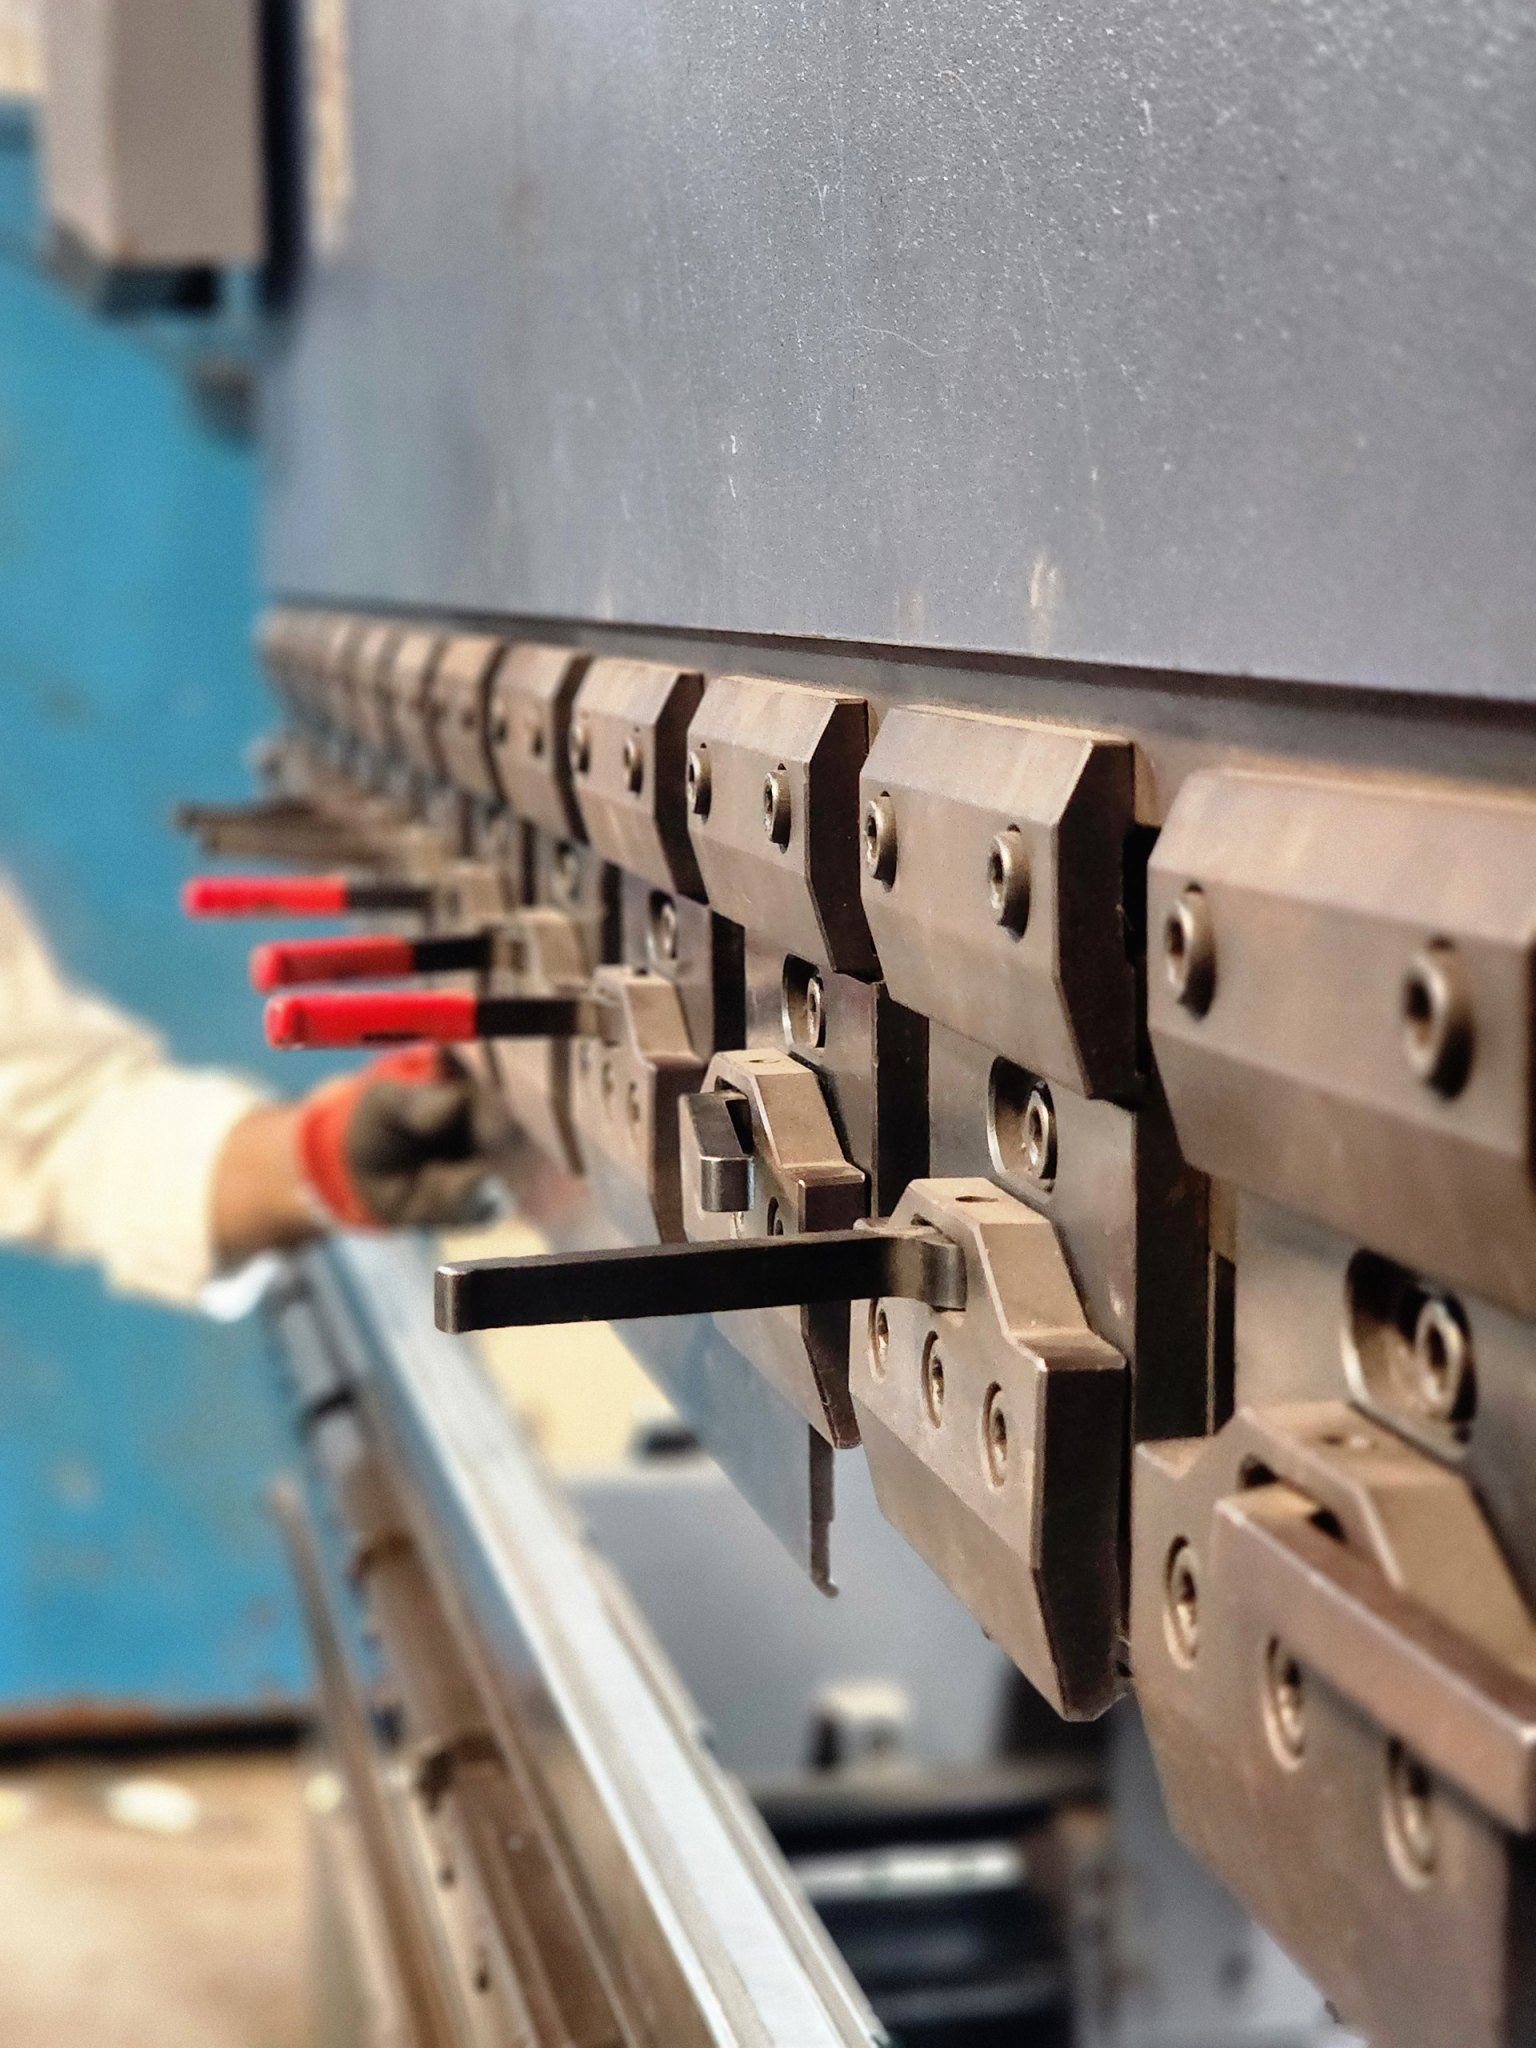
The press brake folds the grooved or plain blank into its section. Its CNC back gauge places the sheet for each bend in turn, so a profile with many bends is folded in the planned order, and every piece of a batch comes out alike. The programme is kept for repeat orders.
Punches and dies are chosen for the section; V-dies are kept ground for sharp-edge bending of V-grooved parts. Sheet from 0.25 to 4 mm is bent and V-grooved.
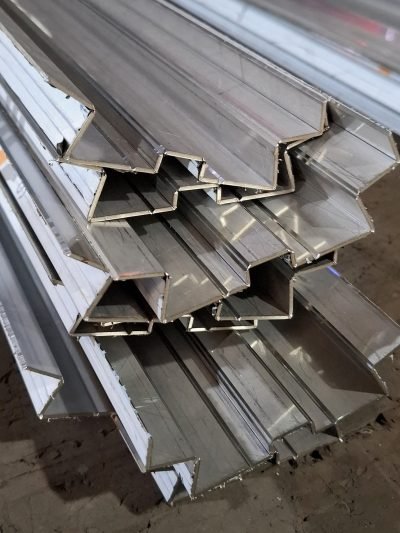
Used for: channels, angles, Z and hat sections, boxes, cassettes and trays, with bends up to 3 m long.
Welding, assembly and finishing
Joined, ground flush
and finished after the fold
Where a part has more than one piece, it is TIG or spot welded, ground flush and assembled on the bench, with drilling where the fixings need it.
The surface is finished after the fold, so edges and corners are finished too: deburring, grinding, buffing, polishing, brushing and bead blasting. PVD colours (on stainless steel 304 and 316) and powder coating are arranged by MCS through approved coating vendors.


Inspection and dispatch
Checked before
anything leaves
Dimensions, grooves, bend angles, surface and finish are checked against the drawing and the approved sample, with measuring tools at the bench and at the press brake.
Parts are then packed, numbered for the order and dispatched from Narela, Delhi to sites across India.
The machines at work
In our
workshop




One part, machine by machine
A 3 m stainless steel U channel,
from sheet to site
An example: a U channel in stainless steel, 3 m long, hairline finish, with sharp corners. This is how it moves through the workshop.
Questions and answers
Machines:
questions
What is the largest part you can make?
It depends on the step: the laser bed is 2 m × 4 m, sheets are V-grooved up to 4 m long and bends are up to 3 m long. For a longer part, send the drawing and we propose where it is joined.
Which thickness can you bend and V-groove?
0.25 to 4 mm, in stainless steel, mild steel, aluminium, brass and copper. Laser cutting goes up to 16 mm mild steel and 8 mm stainless steel.
Do you keep programmes for repeat orders?
Yes. The bending programme is kept, so a repeat batch matches the first.
Can I send only one step, such as laser cutting?
Yes. Send only the step you need, or the complete part.
How do I know my part fits?
Send the drawing. Our design team checks it against the machines, the metal and the thickness before quoting.
Start a project
Check that it fits the machine
Send the section and its length. MCS will confirm that it can be made, before you build the rest of the detail around it.